Automation Engineered for the Complexity of Chemical Processing
Chemical manufacturing demands more than reliable process control. Hazardous atmospheres, corrosive environments, critical reactions, ageing automation systems, complex batch sequences and stringent safety requirements all influence how the control system must be engineered.

CHEMICAL &PETROCHEMICALSOLUTIONS
Our experience includes Sulphuric Acid, Paint Manufacturing, and Dyes & Pigments, supported by capabilities in hazardous-area engineering, SIL 2/SIL 3 Safety Instrumented Systems, legacy-system modernization and control panels engineered for demanding environments.
Engineered Around Process Risk, Not Just I/O Count
Chemical manufacturing brings together process complexity and operating risk. A control system may need to coordinate raw-material transfer, reaction sequences, heating and cooling, dosing, mixing, separation and utilities while managing hazardous-area requirements, process interlocks and functional safety.
Hazardous & Flammable Materials
Automation systems operating around flammable gases, vapours, solvents and combustible materials require appropriate hazardous-area engineering.
Critical Process Reactions
Reliable control and protection are essential where deviations in temperature, pressure, flow or sequence can create process risk.
Corrosive Environments
Panels, enclosures and field interfaces may require appropriate materials and protection for aggressive chemical environments.
Multi-product Manufacturing
Flexible sequencing and recipe-oriented control are essential where shared production equipment is used to manufacture multiple chemical products.
Ageing Automation Infrastructure
Legacy PLC, DCS and operator systems can increasingly affect plant reliability, maintainability and future expansion capabilities.
Changing Global Standards
Chemical plant equipment supplied to India, IEC markets and North America must meet different hazardous-location and control-panel requirements.


CENTRAL CONTROL ARCHITECTURE
Chemical Process PLC & DCS Control Panels
CSE Solutions engineers PLC and DCS control panels for chemical-process applications, integrating process automation, instrumentation, safety requirements and plant interfaces into reliable control-system architectures.
Solutions can be developed for continuous, batch and multiproduct chemical processes, depending on the application and project requirements.
PLC / DCS SYSTEMS
Process control, remote I/O and package-control integration.
SAFETY SYSTEMS
SIL 2 / SIL 3 SIS, safety PLC, trips and interlocks.
HAZARDOUS-AREA APPLICATIONS
Ex p, Ex d and Ex e protection concepts where applicable.
PANEL ENGINEERING
Electrical design, enclosure selection, wiring, testing and documentation.
TECHNICAL CAPABILITIES
Industrial & Automation Control Expertise
CSE Solutions combines automation, safety and electrical engineering capabilities to address the specific control requirements of chemical manufacturing environments.
- 01
PROCESS AUTOMATION
PLC, DCS, HMI/SCADA and industrial communication engineering.
- 02
HAZARDOUS AREA SOLUTIONS
Ex p, Ex d and Ex e engineering for classified environments.
- 03
FUNCTIONAL SAFETY
SIL 2 / SIL 3 Safety Instrumented System capabilities.
- 04
AGEING INFRASTRUCTURE
Zero-first-time swing: 0mm migratory reactor shunt, toxic gas interlocks systems.
- 05
BATCH AUTOMATION
Structured automation approaches for batch, recipe and multiproduct processes.
- 06
HARSH ENVIRONMENT PANELS
Panel engineering considering corrosive exposure, enclosure requirements and environmental conditions.
- 07
PLANT INTEGRATION
Integration across field instrumentation, PLC/DCS, HMI/SCADA and plant systems.
INTEGRATED SOLUTION
Engineered Control Panels for Chemical Operations
Engineered to perform in highly corrosive, explosive, and continuous environments, our panel lineup integrates advanced automation with ergonomic operator control.
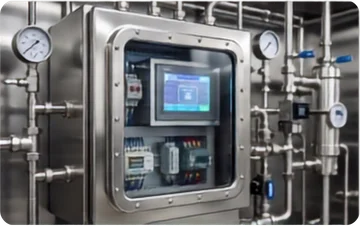
Hazardous-Area Control Panels
Panel solutions engineered around applicable hazardous-area protection concepts including Ex p, Ex d and Ex e.
Explore Hazardous Area Solutions
Safety Instrumented System Panels
Control-panel solutions supporting SIL 2 / SIL 3 SIS, safety PLCs, emergency shutdown, process trips, interlocks and safety I/O.
Explore Safety Solutions
Corrosion-Resistant Control Panels
Panel construction can consider SS304, SS316/SS316L, high-IP protection, corrosion-resistant components and suitable environmental protection, based on actual site conditions.
Discuss Your Panel Requirement
SUCCESS STORY
Case Study: Surfactants Plant Speciality
Modernising legacy automation and integrating SIL 2 safety instrumented systems, with zero unplanned shutdowns
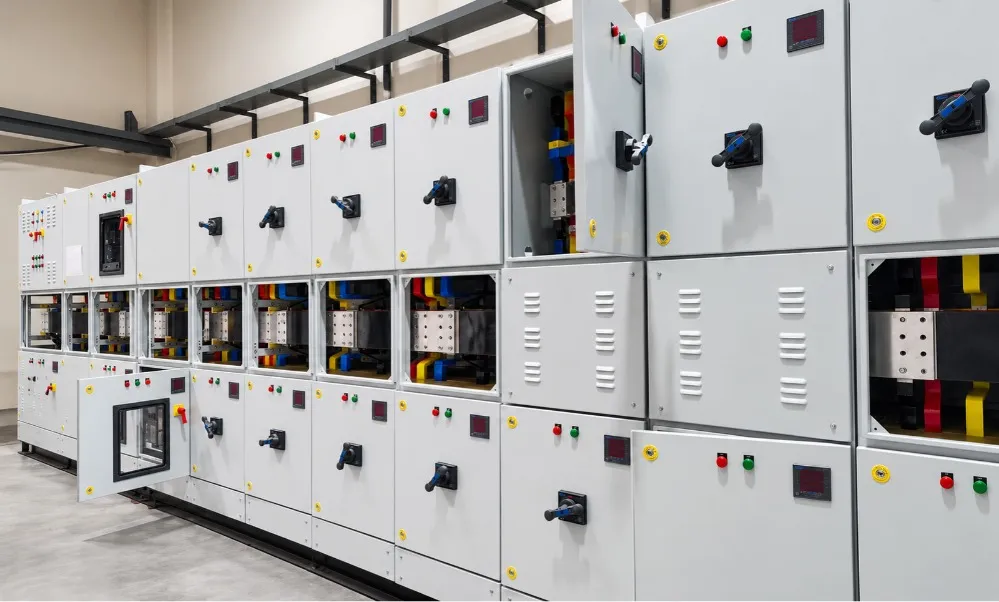
A leading global manufacturer of surfactants and specialty care ingredients, supplying the personal care and beauty industries, required a robust, UL 891-certified Main Power Control Center (PCC) for their new integrated manufacturing facility in Mexico. This was the customer's first experience procuring UL 891 equipment, and also CSE Solutions' inaugural design at this capacity and complexity level. Working as collaborative partners, CSE and the customer navigated the technical and compliance requirements together, resolving challenges through joint problem-solving and iterative design refinement. CSE engineered and manufactured a 4,000 A continuous, 65 kA short-circuit rated switchboard that integrated advanced safety, thermal management, plant-system connectivity and compliance requirements. The system successfully completed factory acceptance testing and has been dispatched to the customer's site for installation and commissioning.
GLOBAL ACCREDITATION
Tested & Certified to Global Chemical Industry Standards
- IEC 61511 | Functional Safety – SIL 2 / SIL 3
- ISA-88 | Structured Batch Automation
- IEC 60079 | Hazardous Area Engineering
- UL 1203 | Explosion-Proof Equipment
- UL 121201 | Hazardous-Location Equipment
- NFPA 496 | Purged & Pressurized Enclosures
Frequently Asked Questions
Chemical Processing FAQs
What automation solutions does CSE Solutions provide for chemical processing plants?
We deliver Chemical plant DCS integration, Batch automation / ISA-88 system integrator India solutions, safety instrumented systems, and explosion-protected field control hardware tailored for chemical manufacturing.
Which company builds Zone 1 purged control panels for chemical and refinery applications?
CSE Solutions is a premier ATEX IECEx Certified Control Panel Manufacturer for Zone 1 Zone 2 providing Purge Control Panel - Ex p, Type X/Y/Z, NFPA 496 systems for chemical hazardous locations.
How does CSE Solutions ensure safety in hazardous chemical environments?
We integrate SIL 2 / SIL 3 SIS Safety Engineering & Integration systems utilizing GuardLogix and Rockwell Logix SIS SIL 3 system integrator India controllers to protect critical chemical process units.
Does CSE Solutions supply hazardous area junction boxes for chemical plants?
Yes, we are a leading Hazardous area junction box / Ex d / Ex e panel manufacturer India, providing Ex d / Ex e junction boxes and panels Zone 1 / Zone 2 in stainless steel and cast aluminum.
How does CSE Solutions execute legacy system migration in continuous chemical processes?
We provide Control System Migration / PLC-5 / SLC Migration & Modernization Services to upgrade aging PLC architectures to PlantPAx DCS without causing unplanned process downtime.
.png)
.png)
.png)
.png)
.png)
.png)